Direct-from-factory engineering solutions engineered for hospitality, luxury residential, and wholesale distribution networks. Built with kiln-dried timber, precision hardware, and integrated luxury tops.
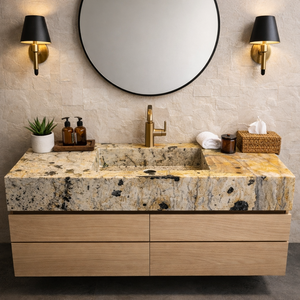
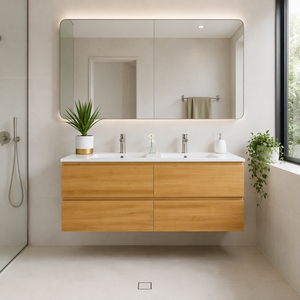
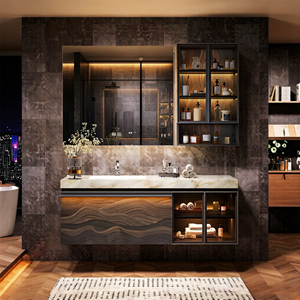
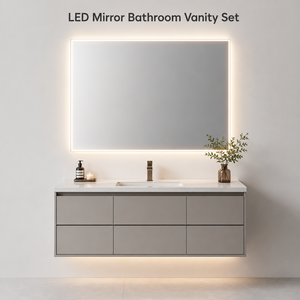
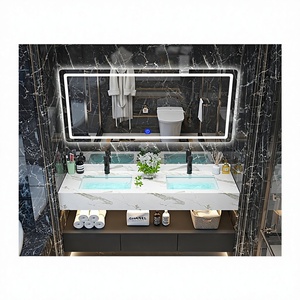
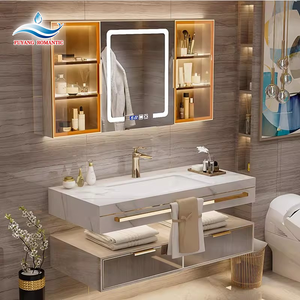
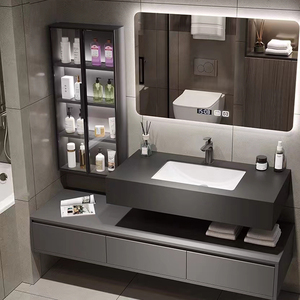
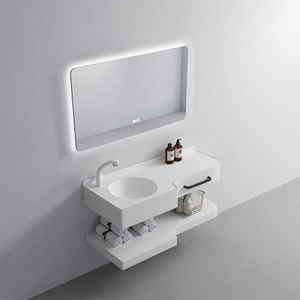
In the global hospitality, commercial construction, and retail distribution markets, the demand for rustic solid wood vanity cabinets has experienced an unprecedented surge over recent years. Architects, procurement managers, and wholesale importers are increasingly looking toward specialized OEM/ODM manufacturing hubs in China to supply high-end, durable, and architecturally striking bathroom millwork. This whitepaper analyzes the manufacturing methodologies, technical timber treatment benchmarks, global supply chain dynamics, and product engineering frameworks required to evaluate elite China vanity suppliers.
Key Information Gain Insight: True commercial-grade solid wood vanities are defined by timber moisture equilibrium, zero-VOC sealing, multi-layer joinery, and structural load-bearing frame ratings exceeding 150 kg for floating installations.
The single greatest cause of wood deformation, grain splitting, or frame expansion in North American and European climates is improper timber drying. China’s premier solid wood vanity factories utilize automated computer-controlled dehumidification kilns. Raw timbers—such as North American Red Oak, White Ash, Solid Walnut, Pine, and Teak—undergo a multi-week thermal seasoning protocol.
For export to dry climates (such as the US Southwest or Western Europe), timber moisture content must be rigidly locked between 8% and 10%. For humid coastal zones, the moisture threshold is maintained between 10% and 12%. Advanced vacuum thermal treatment (thermo-treated wood) neutralizes internal stresses, eliminating fiber movement prior to CNC precision cutting.
Multi-stage computer controlled thermal vacuum drying eliminates wood stress and prevents warping, cracking, or grain lifting across varied climate zones.
Automated 5-axis woodworking machinery creates seamless mortise-and-tenon framing and solid wood English dovetail drawer boxes.
7-layer polyurethane micro-sealing process delivers 100% moisture resistance, protecting against vapor penetration and chemical staining.
When selecting cabinetry for high-traffic hotel contracts or luxury residential projects, commercial buyers must balance aesthetic authenticity, structural strength, moisture resistance, and cost parameters.
| Substrate Grade | Moisture Resistance | Tensile Strength | Eco-Standard / Emission | Best Application Fit |
|---|---|---|---|---|
| Solid Oak / Ash / Walnut | High (7-Layer Sealed) | Extreme (High Hardness) | FSC Certified / Zero VOC | Luxury Hospitality & Premium Retail |
| Thermo-Treated Pine | Very High (Stable Core) | Medium-High | CARB Phase 2 / TSCA VI | Rustic & Modern Farmhouse Collections |
| Marine Plywood (P2 Core) | Maximum (Cross-Laminated) | Very High | E0 Grade Standard | High-Humidity Commercial Bathrooms |
| Standard MDF / Particleboard | Low-Medium (Swell Risk) | Moderate | E1 Grade Standard | Budget Multi-Family Housing |
The global bathroom furniture ecosystem is undergoing a dramatic structural migration towards smart, integrated luxury floating vanity systems. Modern interior design favors clean, wall-mounted floating silhouettes that maximize floor area while introducing natural organic textures like wire-brushed oak, reclaimed timber, and quartzite surfaces.
Conventional drop-in ceramic basins are rapidly being replaced by monolithic engineered quartz tops, natural Pandora quartzite slabs, and solid resin stone sinks with integrated continuous slopes. The seamless union between rustic solid wood bases and quartz stone tops prevents water accumulation at seams, significantly extending cabinet lifespan in hotel environments.
Commercial vanity packages are no longer sold as standalone cabinets. Procurement orders overwhelmingly specify turnkey vanity bundles including Smart LED Mirrors. Key specs include high color rendering index (CRI > 90), integrated anti-fog heating elements, touch dimming actuators, and ambient backlight kelvin adjustment (3000K-6000K).
Leveraging state-of-the-art production facilities, our partner factory network embodies the highest level of industrial execution. Trusted by North American distributors, European contract buyers, and global hotel brands, the factory bridges luxury design with accessible factory-direct pricing.
Clear, direct technical answers addressing the critical commercial, quality control, and logistical queries of B2B vanity procurement.
We utilize automated computer-controlled kiln drying to lock wood moisture content strictly between 8% and 12%. Combined with multi-layer sealing and cross-grained stress release cuts on cabinet backs, structural stability is guaranteed under extreme climate shifts.
Our raw timber complies with FSC and CARB Phase 2 / TSCA Title VI standards for formaldehyde emissions. Smart LED mirrors and electrical components carry UL, ETL, CE, and RoHS approvals for safe international installation.
Our baseline MOQ for custom OEM/ODM production is 10-20 units per SKU, or full 20GP/40HQ mixed-container orders. Lead times range from 30 to 45 days upon CAD specification approval.
Yes. Our wall-mounted floating vanities feature heavy-duty powder-coated steel back brackets and reinforced internal solid wood framing, tested to support downward static loads up to 200 kg (440 lbs).
We equip our cabinets with top-tier DTC or BLUM concealed soft-close drawer slides and 110-degree 3D adjustable soft-close hinges, certified for over 100,000 smooth cycle operations.
All vanity units are packed using ISTA-3A standardized drop-test packaging, featuring high-density honeycomb corner protectors, molded EPE foam barriers, and heavy-duty 7-ply corrugated outer master cartons.
Connect directly with our engineering team to review full specs, material sample swatches, price tiers, and project references for hotel and residential developments.
Get Catalog